Nantong Alisen Environmental Protection Technology Co., Ltd.
Nantong Alisen Environmental Protection Technology Co., Ltd. is a
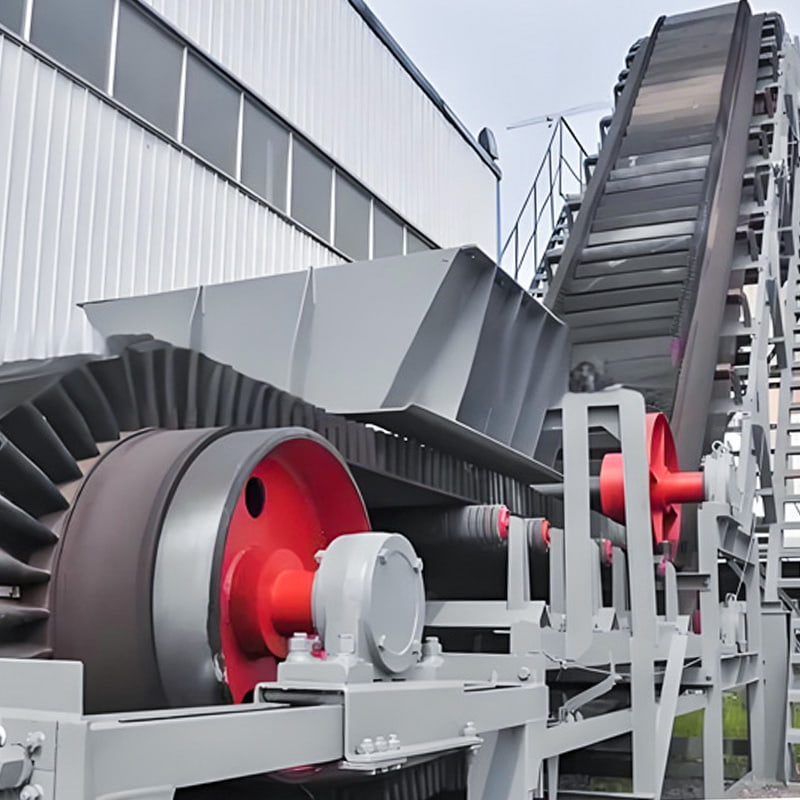
China TD Belt Conveyor Manufacturers for Fertilizer/Powder Production Equipment and
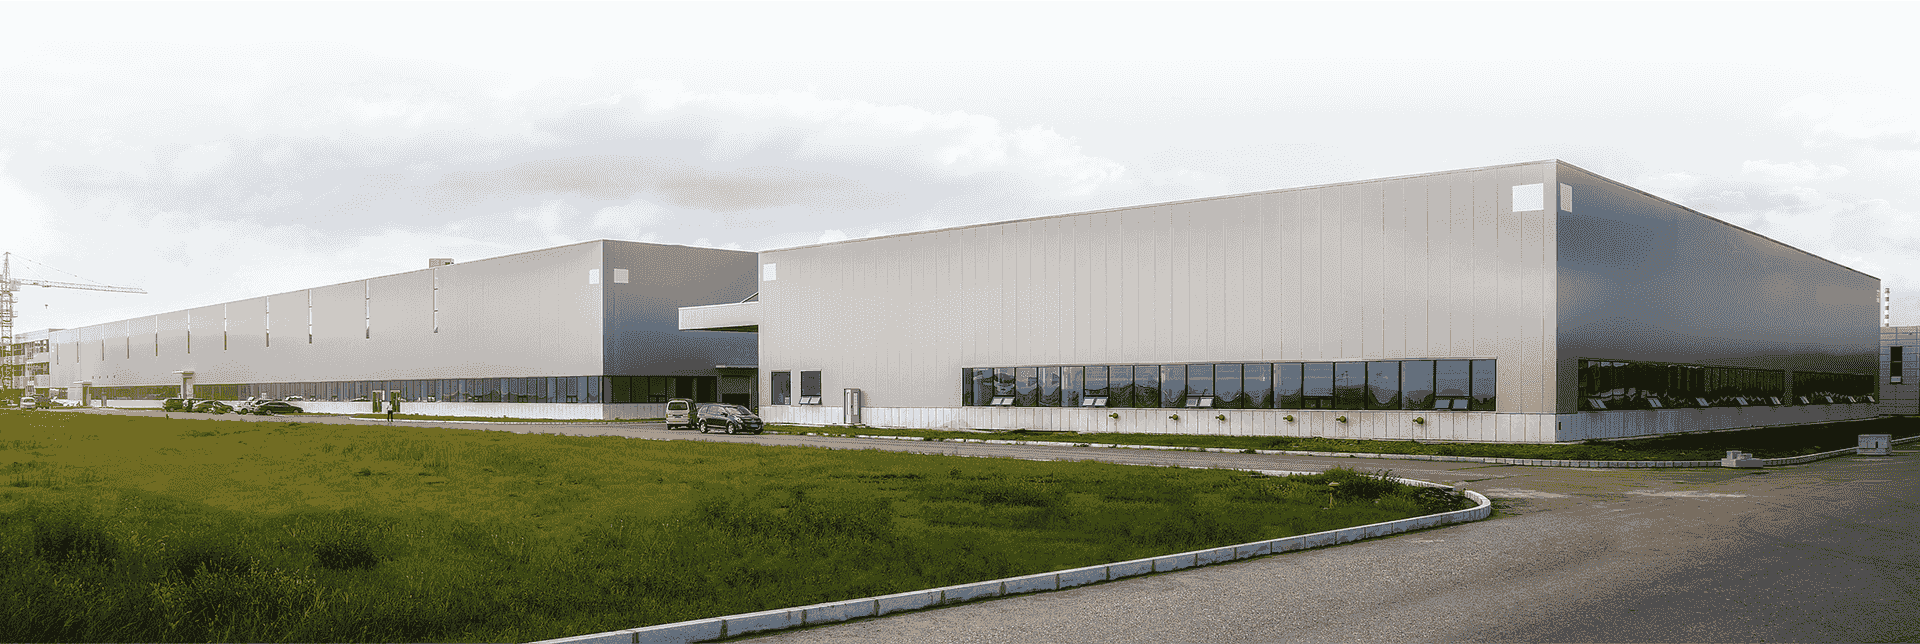
Custom TD Belt Conveyor Factory. Founded in 2007, Nantong Alisen Environmental Protection Technology Co., Ltd. is located in Qutang Town Industrial Park, Haian City, Jiangsu Province. It has two wholly-owned subsidiaries, namely Nantong alisen Import and Export Co., Ltd. and Nantong Ailisen Environmental Protection Technology Co., Ltd. As a technology-oriented company focusing on fertilizer machinery and building materials machinery, we have been committed to the design and manufacturing of various types of fertilizer machinery and building materials machinery for many years.
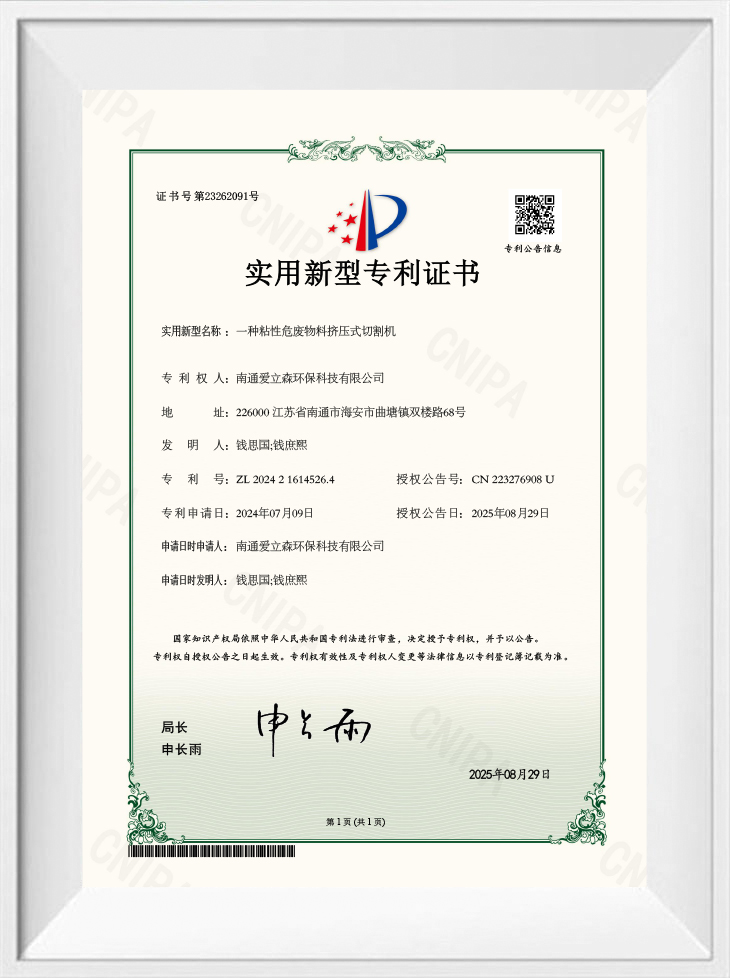
The company boasts strong design and development capabilities, with its products covering a wide range and featuring high technological content. Many of its products lead the industry both domestically and internationally.
Its main products include TD Belt Conveyor, rotary kilns, drum granulators, dryers, coolers, coating machines, crushers, conveyors, dust collectors and other equipment, which are widely used in major chemical fertilizer manufacturers. These products are applied in complete production lines for compound fertilizers, organic fertilizers, bulk blending fertilizers (BB fertilizers), potassium sulfate, etc.
With experienced technicians and mature process design concepts, the company can provide users with a full set of services, including process design for compound (mixed) fertilizer complete sets, equipment production, formula customization, equipment installation and on-site training. While supplying users with a full set of equipment, the company also provides technical upgrading and transformation services in terms of new production capacity and environmental protection for old fertilizer production enterprises.
Adhering to the business philosophy of "Customer First, Quality-Oriented, Reputation as Solid as a Tripod, and Service Supreme", the company strives to meet the personalized needs of customers and provide high-quality services. It takes customer satisfaction as the criterion for measuring the enterprise, thus winning the trust and support of a large number of customers. At the same time, we warmly welcome experts and colleagues at home and abroad to visit for guidance, discuss cooperation and create a better future together.
 En
 English
 Français
 русский
 中文简体
 عربى
 Español